

How to Inspect Plywood Quality Before Shipment: A Buyer’s Checklist
Quick answer: A useful pre-shipment inspection compares the finished plywood with the purchase order, approved sample and agreed inspection criteria. Buyers should check dimensions, moisture condition, core and bonding quality, surface workmanship, quantity, packing and container loading before approving shipment.
The acceptance criteria should be agreed before production. Different products—such as furniture plywood, packing plywood, marine plywood and film faced plywood—may require different tolerances, grades, bond performance and packing methods.
1. What Should Be Confirmed Before Inspection?
An inspector needs a clear reference. Prepare the purchase order, product specification, approved sample or photos, packing requirements and any agreed test method. Confirm the product name, face and back grade, core construction, glue or bonding requirement, size, thickness, quantity, marking and intended application.
Avoid using only general descriptions such as “good quality” or “export grade.” A measurable specification makes the final decision clearer for both buyer and supplier.
2. How Should Dimensions and Thickness Be Checked?
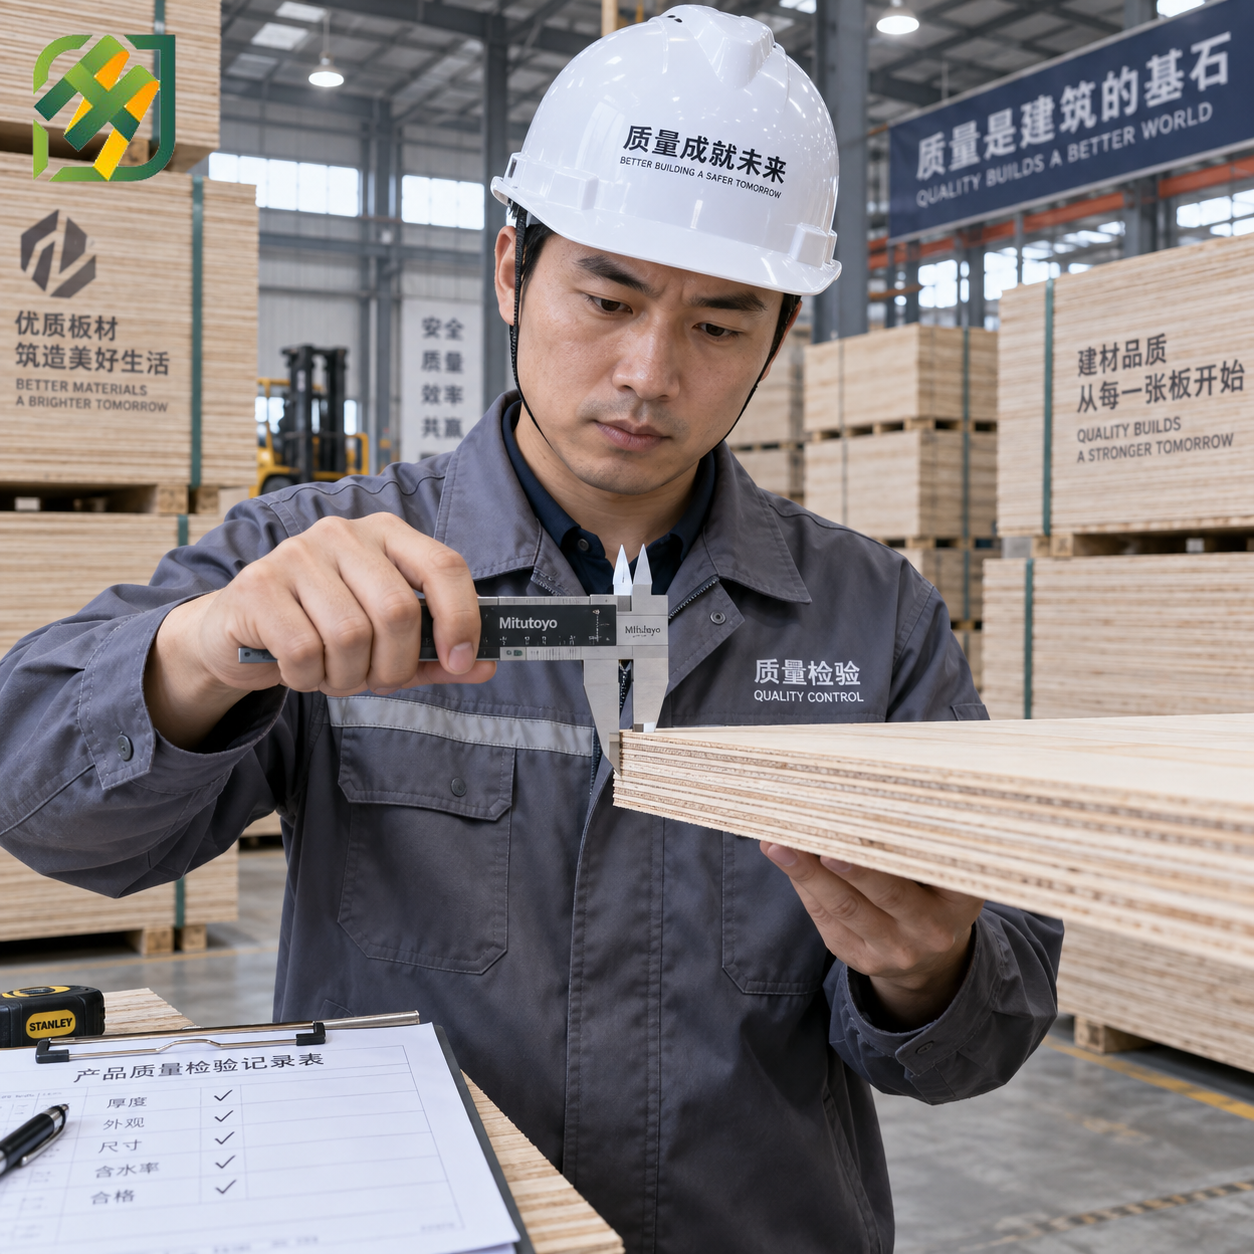
Use suitable calibrated tools to measure length, width and thickness. Select sheets from different pallets and different positions instead of checking only the top panels. Thickness should be measured at several agreed points because an average value can hide local variation.
- Confirm nominal length, width and thickness against the order.
- Check squareness by comparing diagonals or using the agreed method.
- Inspect edge straightness and panel flatness.
- Record individual readings and identify the pallet or batch.
ISO 9426 describes methods for measuring panel thickness, width, length, squareness, edge straightness and flatness.[1] The actual acceptance tolerance should still follow the confirmed order or applicable product standard.
3. How Should Moisture Condition Be Reviewed?
Moisture condition can affect panel flatness, dimensional stability, surface appearance and transport risk. Take readings from multiple sheets, pallets and positions with an appropriate moisture meter. Record the instrument type, settings and measurement locations so the results can be reviewed consistently.
A handheld meter is useful for shipment screening, while a reference laboratory method may be required when the contract, standard or dispute requires a formal result. The acceptable moisture range should be agreed for the specific plywood type and destination conditions rather than assumed from one universal figure.
4. How Can Buyers Check Core and Bonding Quality?
Inspect panel edges and, when agreed, cross-cut samples from representative pallets. Look for open glue lines, visible delamination, large core gaps, overlapping veneers and construction that does not match the approved specification.
Bonding quality should be evaluated using the method agreed for the product and intended use. ISO 12466-1 specifies shear-test methods for determining the bonding quality of plywood and related panels bonded with thermosetting resin.[2] Do not replace a required laboratory or contract test with an informal field test.
5. Which Surface and Edge Defects Should Be Checked?
Surface acceptance depends on the ordered grade and application. Furniture panels may prioritize smooth sanding, color consistency and repair quality, while film faced plywood requires inspection of the film surface, corners and edges.
- Check both faces for splits, open knots, patches, stains, scratches and press marks.
- Check whether repairs and color variation match the agreed grade or sample.
- Inspect edges for chipping, crushing, open layers and core gaps.
- For overlaid panels, check film condition and edge sealing when specified.
6. What Should Be Checked in Packing and Marking?
Verify the number of sheets per package and the total number of packages against the purchase order and packing list. Check pallet condition, bottom supports, protective wrapping, straps, edge protectors and shipping marks.
Labels should identify the product, size, thickness, quantity and other information agreed for the order. Requirements for wood packaging treatment, marks and supporting documents should follow the destination market and shipping agreement.
7. Which Container-Loading Evidence Should Buyers Request?
Before loading, check that the container is clean, dry and suitable for the shipment. The loading arrangement should keep packages stable and reduce the risk of movement, crushed edges or contact with moisture during transport.
A practical loading record can include photos of the empty container, container number, package labels, loading stages, final arrangement, closed doors and seal number. This creates a clearer record of which goods were loaded and how the container was released.
8. Final Plywood Inspection Checklist
- Product specification matches the purchase order and approved sample.
- Length, width, thickness, squareness and flatness meet the agreed criteria.
- Moisture readings are recorded across representative samples.
- Core construction and bonding match the ordered product.
- Surface grade, edges and repairs meet the agreed standard.
- Sheet count, package count, labels and packing list agree.
- Packing and container condition are suitable for shipment.
- Inspection findings, photos and release decision are documented.
ISO 12465 covers plywood specification topics including veneer quality, glue bond, construction, dimensions and tolerances, conformity verification and marking.[3] Buyers should select the inspection basis that applies to the exact product, end use and destination market.
Send Your Plywood Requirement
Review Haoxin’s plywood products and factory information. Tell us your required plywood type, size, thickness, core, face grade, glue requirement, quantity, packing and destination port. Haoxin will provide a suitable quotation and discuss the inspection requirements for your order.
Contact Haoxin for plywood specifications, pricing and shipment details.